
Rebar Straightening and Cutting Machine Guide (YGT4-15A)
Rebar Straightening and Cutting Machine Guide: YGT4-15A
If your fabrication shop still buys coiled rebar and cuts it by hand, or runs straightening and cutting as two separate operations, you are paying for it twice — once in labour and once in wasted bar. The YGT4-15A from Gongda (China Rebar Machinery) is a combined straightening and cutting machine built for 4–15 mm rebar and wire, and it is one of the most practical entry points into automated rebar processing for precast plants, mesh producers, and general fabrication yards.
What the YGT4-15A Actually Does
The machine takes coiled rebar or wire rod, pulls it off the coil, runs it through a multi-roll straightening block, and then cuts it to a preset length in a single continuous pass. The operator sets the cut length on the control panel, and the machine feeds, straightens, and shears automatically until the coil is finished or the batch count is reached.
Key specifications worth noting before you buy:
- Working range: 4–15 mm diameter (round bar and deformed rebar)
- Drive: Variable frequency drive (VFD) for stepless speed control
- Function: Straightening and cutting in one pass, no secondary handling
- Cut length: Set digitally; typical accuracy within ±2–3 mm on well-maintained units
- Application: Coiled rebar, wire rod, and small-diameter straight bar
The VFD is not a marketing detail. On a fixed-speed machine, changing from 6 mm to 14 mm bar means changing pulley ratios or accepting poor straightness on the smaller sizes. With a VFD, the operator dials the line speed down for thick bar and up for thin wire, which keeps the straightening rolls engaged correctly and protects the shear from overload.
Why One-Pass Straightening and Cutting Matters
Separating straightening and cutting into two machines introduces a handling step: straightened bar has to be stacked, moved, measured, and cut. Every transfer bends bar ends, creates scrap, and consumes floor space. On a combined unit like the YGT4-15A, the bar is cut while it is still under tension in the straightening block, so the cut end stays square and the length stays consistent across the batch.
For shops producing stirrups or mesh, this matters because downstream machines — a GW25 single-head stirrup bender or a ZD-6M-25 five-head stirrup machine — perform best with straight, accurately cut stock. Feeding bent or short-length bar into a stirrup bender causes misfeeds and wasted cycles.
Practical Setup Advice
Match coil size to your floor layout
The YGT4-15A pulls from a coil, so you need a decoiling stand or turntable positioned so the bar feeds into the straightener without kinking. Allow at least 1.5–2 m of free run between the coil and the feed rollers. If the coil is placed too close, the bar enters the straightener under lateral load and straightness suffers.
Set the VFD speed to the bar diameter
As a rule of thumb, run slower for 12–15 mm bar and faster for 4–8 mm wire. Pushing a 14 mm bar at wire speeds overloads the shear and shortens blade life. The VFD lets you find the sweet spot without mechanical changes.
Check straightening roll pressure regularly
Straightness quality comes from roll pressure, not from speed. Re-check the roll gap whenever you change bar diameter. A quick test: cut three bars, lay them on a flat surface, and check for bow. If the bow exceeds your tolerance, adjust the roll block before continuing.
Keep the shear blades sharp and aligned
Dull blades produce burred ends and can pull the bar offline, which throws off cut length. On high-volume runs, inspect blades weekly. The YGT4-15A shares blade geometry principles with Gongda's heavier cutting machines like the GQ50A (6–50 mm round / 6–36 mm ribbed) and GQ70A (70 mm, 160-ton shear force), so blade maintenance habits transfer across the range.
Where the YGT4-15A Fits in a Full Line
Think of the YGT4-15A as the front end of a rebar processing line. Straightened and cut bar feeds into:
- Stirrup bending: GW25 (single-head, round steel up to 25 mm) or ZD-6M-25 / ZD-6M-20 five-head machines for high-volume stirrup production
- CNC bending: GJZD6-50CZ (up to 50 mm, 420 mm working table) or GJZD6-65CZ (up to 65 mm) for complex shapes
- Arc bending: GWH50CG / GWH50CZN (50 mm) or SKDZWH-36 / GDWHWQ-36 (36 mm) for curved sections
- Bending centers: GDLWZX-32 vertical (32 mm) or GDPMW-60 plane (60 mm) for large-format work
- Shearing lines: GDQX-500 hydraulic rebar shearing production line for heavy-duty cutting
For thread rolling and welding operations, the same cut stock feeds the HGS-40 thread rolling machine (40 mm) and NB-350 / NB-500 MIG/CO2 welders. Gongda also builds the GD-350ZD band saw (350 mm) and ZDTHJ-12 automatic spring making machine (12 mm) for shops with broader steel processing needs.
Export and Compliance Notes
Gongda equipment ships worldwide, with established installations in Russia, Spain, Latin America, the Middle East, Southeast Asia, and Africa. EAC certification is available for Russian and CIS markets, which matters if you are importing into a customs union that requires it. Confirm voltage and frequency requirements (380 V/50 Hz vs. 440 V/60 Hz) at the order stage, and specify whether you need a decoiling stand included.
Buying Checklist
- Confirm your bar range: the YGT4-15A covers 4–15 mm. If you regularly run above 15 mm, step up to a heavier straightening and cutting configuration.
- Ask for the cut-length tolerance in writing for your specific diameter mix.
- Specify coil weight and diameter so the decoiler matches.
- Request spare shear blades and straightening rolls with the initial order — downtime on a single machine stops the whole line.
- Confirm EAC documentation if you are importing into Russia or CIS countries.
For pricing, configuration, and shipping to your port, contact the Gongda export team directly: WhatsApp +86 193 9277 7259 or email yuhua0095@gmail.com. Send your bar diameters, target cut lengths, and daily output so the team can confirm whether the YGT4-15A is the right fit or whether a larger straightening and cutting setup is warranted.
Send your requirement on WhatsApp — we reply within one business day.
WhatsApp Request a Quote →Products
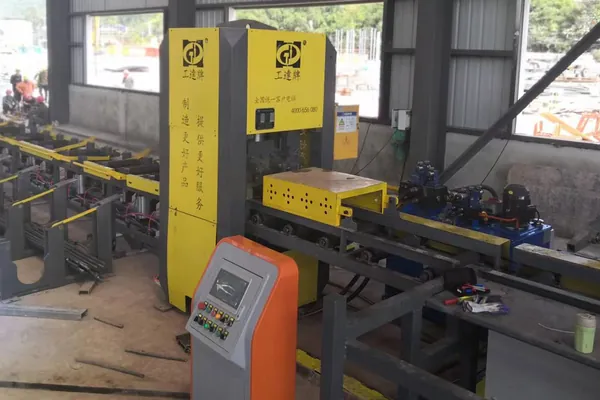
Hydraulic Rebar Shearing Production Line
High-capacity hydraulic rebar shearing production line for cutting ribbed and round bars in mass production.
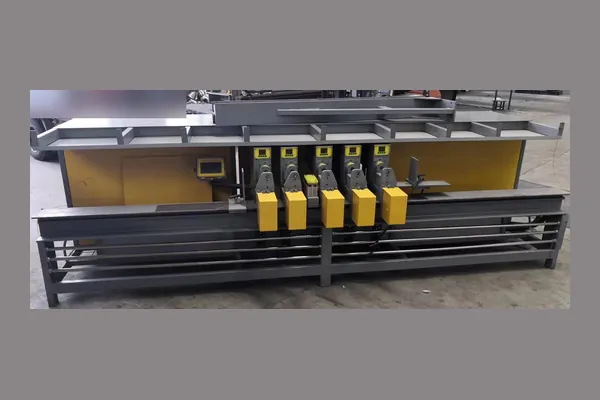
CNC Straightening-Cutting-Stirrup Line
Complete CNC straightening-cutting-stirrup production line combining VFD straightening, hydraulic cutting and five-head stirrup bending.
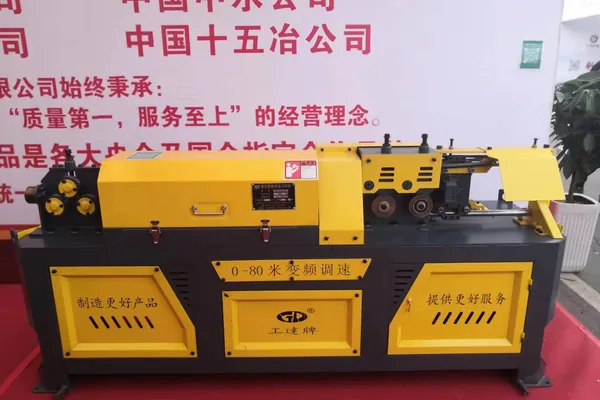
VFD Rebar Straightening & Cutting Machine
VFD-controlled rebar straightening and cutting machine for 4-15 mm bars with hydraulic cutting and ±5 mm accuracy.
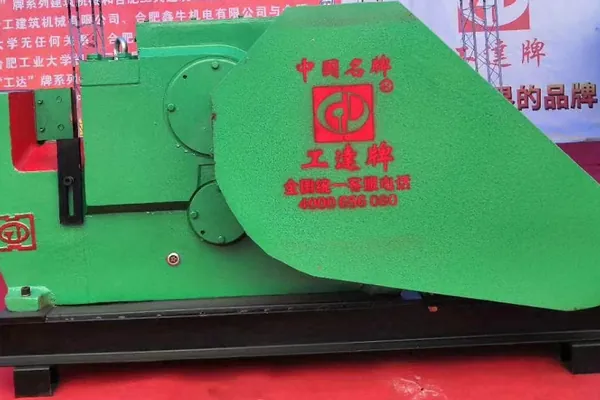
Rebar Cutting Machine
Powerful rebar cutting machine for bars up to 70 mm (A3 round steel) with 160-ton shear force.
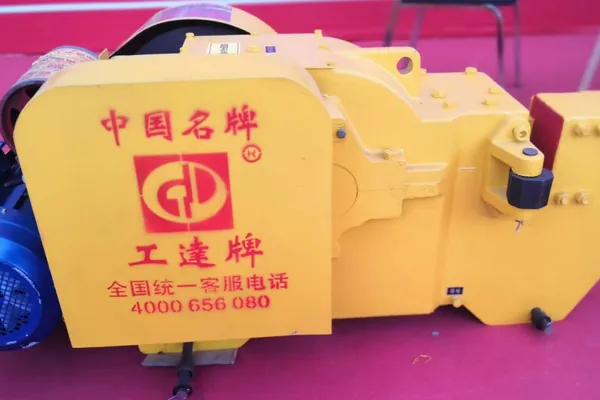
Rebar Cutting Machine
Rebar cutting machine for 6-50 mm round and 6-36 mm ribbed bars, built for daily site and shop use.
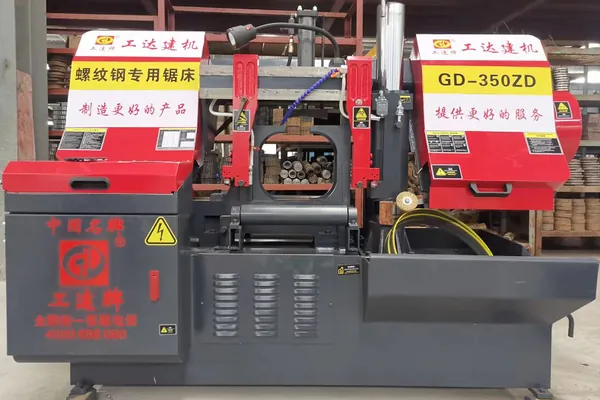
Rebar Band Sawing Machine
Rebar band sawing machine for threaded steel with a 400×350 mm cutting range.
More Articles

Single-Line vs Double-Line Rebar Machines: Which to Choose
Single-Line vs Double-Line Rebar Machines: Which to Choose If you are specifying a CNC rebar forming machine f…

Rebar Machine Electricity Requirements (380V, 50/60Hz)
Rebar Machine Electricity Requirements: 380V, 50/60Hz, and Generator Sizing for Remote Sites Most buyers sourc…
How to Calculate Rebar Processing Productivity
How to Calculate Rebar Processing Productivity: Bends Per Hour, Stirrups Per Shift, and Line Throughput Most b…

Rebar Machine Safety Operation Rules
Rebar Machine Safety Operation Rules: A Practical Guide for Buyers and Operators Rebar processing equipment is…
Rebar Machine Maintenance Checklist
Rebar Machine Maintenance Checklist: Daily, Weekly and Monthly Schedules That Prevent Downtime Every hour a CN…
CNC Stirrup Machine Cost and ROI Calculation
CNC Stirrup Machine Cost and ROI Calculation: What Buyers Should Actually Model When a fabrication shop or reb…
Ready to Talk Numbers?
Send us your rebar processing requirements and get a factory-direct quotation within one business day.